Making an Inspection Setup Work on a Real Production Line

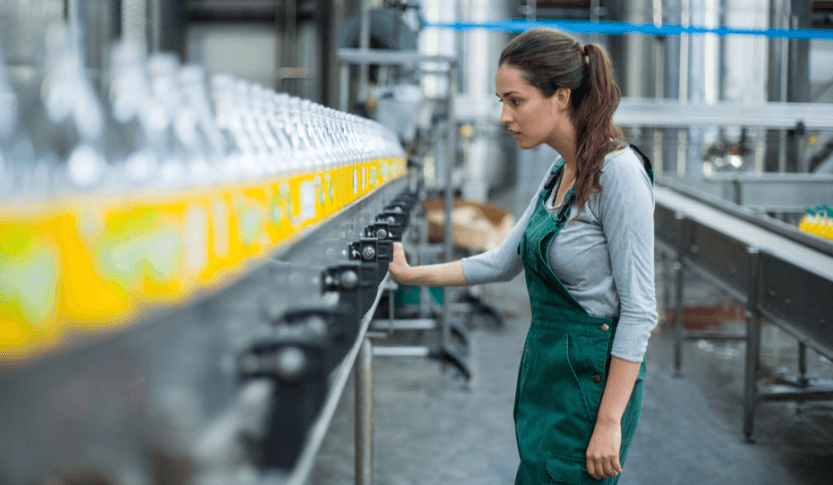
There is a consistent pattern in failed inspection projects. The technology worked in evaluation. The vendor demonstrated it convincingly. The sample parts were classified correctly. And then it was installed on the line, and the false rejection rate made it unusable, or it missed defects it had caught reliably during the trial.
The cause is almost never the algorithm. It is that a production environment differs from an evaluation environment in ways that matter enormously to a camera: ambient light changes through the day, parts arrive at varying positions, vibration moves things slightly, and the surfaces themselves vary more than the sample set suggested.
Getting visual inspection systems to perform reliably is therefore largely about the physical setup and the conditions around the camera, rather than about the sophistication of what happens after the image is captured. A good image makes the analysis straightforward; a poor one makes it nearly impossible.
Lighting Determines Almost Everything
Lighting is the single most important variable and the one most often treated as an afterthought.
The purpose of lighting is to make the feature of interest visible and distinct from everything else. That is a different objective from illuminating the part generally.
Different techniques suit different defects. Directional lighting at a shallow angle reveals surface texture and scratches by casting shadows. Diffuse lighting minimizes shadows and reflections for printed surfaces. Backlighting produces silhouettes for dimensional measurement. Coaxial lighting suits reflective surfaces where specular reflection is otherwise overwhelming. Structured light reveals surface geometry.
Choosing wrongly makes defects invisible regardless of what happens downstream.
Consistency matters as much as technique. Ambient light changing through the day, or when a bay door opens, introduces variation that the system reads as a change in the part. Enclosing the inspection area is frequently the single most effective improvement available.
Light source aging is a slow failure mode that degrades performance gradually and is easy to miss. Scheduled replacement prevents a mysterious decline in accuracy months after installation.
Camera and Optics Choices
The imaging hardware has to suit the inspection rather than being selected on specification alone.
Resolution should be determined by the smallest feature that must be detected, with enough pixels across that feature for reliable identification. More resolution than necessary increases cost and processing load without improving results.
Sensor type matters for moving parts. Area sensors capture a frame; line sensors build an image as material passes and suit continuous webs and cylindrical surfaces.
Exposure and shutter behaviour determine whether moving parts appear sharp or blurred, and motion blur destroys fine defect detection.
Lens selection affects field of view, working distance, and depth of field, and a lens chosen without regard to the mounting constraints causes problems that are expensive to fix afterwards.
Colour versus monochrome depends on whether colour information carries meaning. Monochrome sensors generally offer better resolution and sensitivity for the same cost when colour is not required.
Mounting rigidity is unglamorous and important. A camera that moves slightly with line vibration produces images that vary for reasons unrelated to the parts.
Part Presentation
How the part arrives in front of the camera affects results more than most implementations account for.
Positional consistency simplifies everything. A part that appears in the same place and orientation every time allows tight analysis; one that varies requires the system to locate it first and tolerate the variation.
Fixturing that constrains position is cheaper than software that compensates for its absence.
Surface condition affects imaging. Oil, coolant, dust, and handling marks all change appearance, and a system trained on clean parts performs differently on the line.
Speed determines exposure requirements and whether the part is effectively stationary during capture.
Multiple views are needed where defects can occur on surfaces a single camera cannot see, and deciding this early prevents a system that inspects one face well and misses the others entirely.
Integrating With the Line
A system that identifies defects and cannot act on them delivers a fraction of its value.
Triggering has to be reliable, meaning the system captures at the right moment, usually from a sensor detecting part presence rather than on a timer.
Rejection mechanisms need to remove identified parts reliably and to be verified, since a reject mechanism that occasionally fails undermines the entire inspection.
Cycle time has to accommodate capture, processing, and decision within the available window, and a system that cannot keep up either slows the line or skips parts.
Data connection to quality systems turns inspection into process information rather than a pass or fail gate.
Operator interface matters. The people running the line need to see what is happening, understand why parts were rejected, and handle exceptions, and an opaque system loses their trust quickly.
Validating Before Trusting
Validation deserves more effort than it usually receives.
Test with known samples covering both good parts and the full range of defects, including marginal cases rather than only obvious ones.
Measure the two error types separately. False negatives, meaning defects that pass, and false positives, meaning good parts rejected, have very different costs and a single accuracy figure hides the balance between them.
Run across conditions: different shifts, different material lots, different times of day, and after a line changeover.
Compare against current inspection performance rather than against perfection, since the relevant question is whether this is better than what happens now.
Involve the inspectors, who will identify the cases the system handles badly faster than any test protocol.
Keeping It Working
Performance degrades quietly unless someone is watching.
Lighting ages, lenses accumulate film, and mounting drifts. A cleaning and verification schedule prevents a slow decline that nobody attributes to the hardware.
Reference parts run periodically confirm that the system still classifies known samples correctly.
Rejection rate trends are the most useful ongoing indicator. A rate that moves without an obvious process change usually means the system has drifted rather than the product.
Process and material changes should trigger a review, since a system configured for one supplier’s material may behave differently with another’s.
And someone should own it. Inspection systems that nobody is responsible for are the ones found six months later running with a fouled lens and a rejection rate nobody has examined.